 English
 Korean


The appliance and electronics segment consumed 63% of ABS resin in 2025, with air-conditioner panels and refrigerator liners among the largest single applications. The styrene copolymer market reached USD 27 billion that year, expanding at roughly 7.4% annually, with Asia-Pacific growing faster at 8%. This volume growth has not made material selection simpler. White appliance housings now carry tighter expectations on long-term colour stability, lot-to-lot consistency, and UV performance than the general-purpose grades of the previous decade. Dye colour ABS for white appliance housings sits at the centre of that shift: the base polymer must process predictably, and the dye colour system must hold through a five-hundred-hour accelerated weathering cycle without drifting outside the customer's ΔE window. Chimei PA-757 A01 has functioned as an industry reference point for this application. What follows is a practical qualification framework for evaluating a dye colour ABS grade against that benchmark, drawn from compounding and field-verification experience rather than datasheet comparison alone.
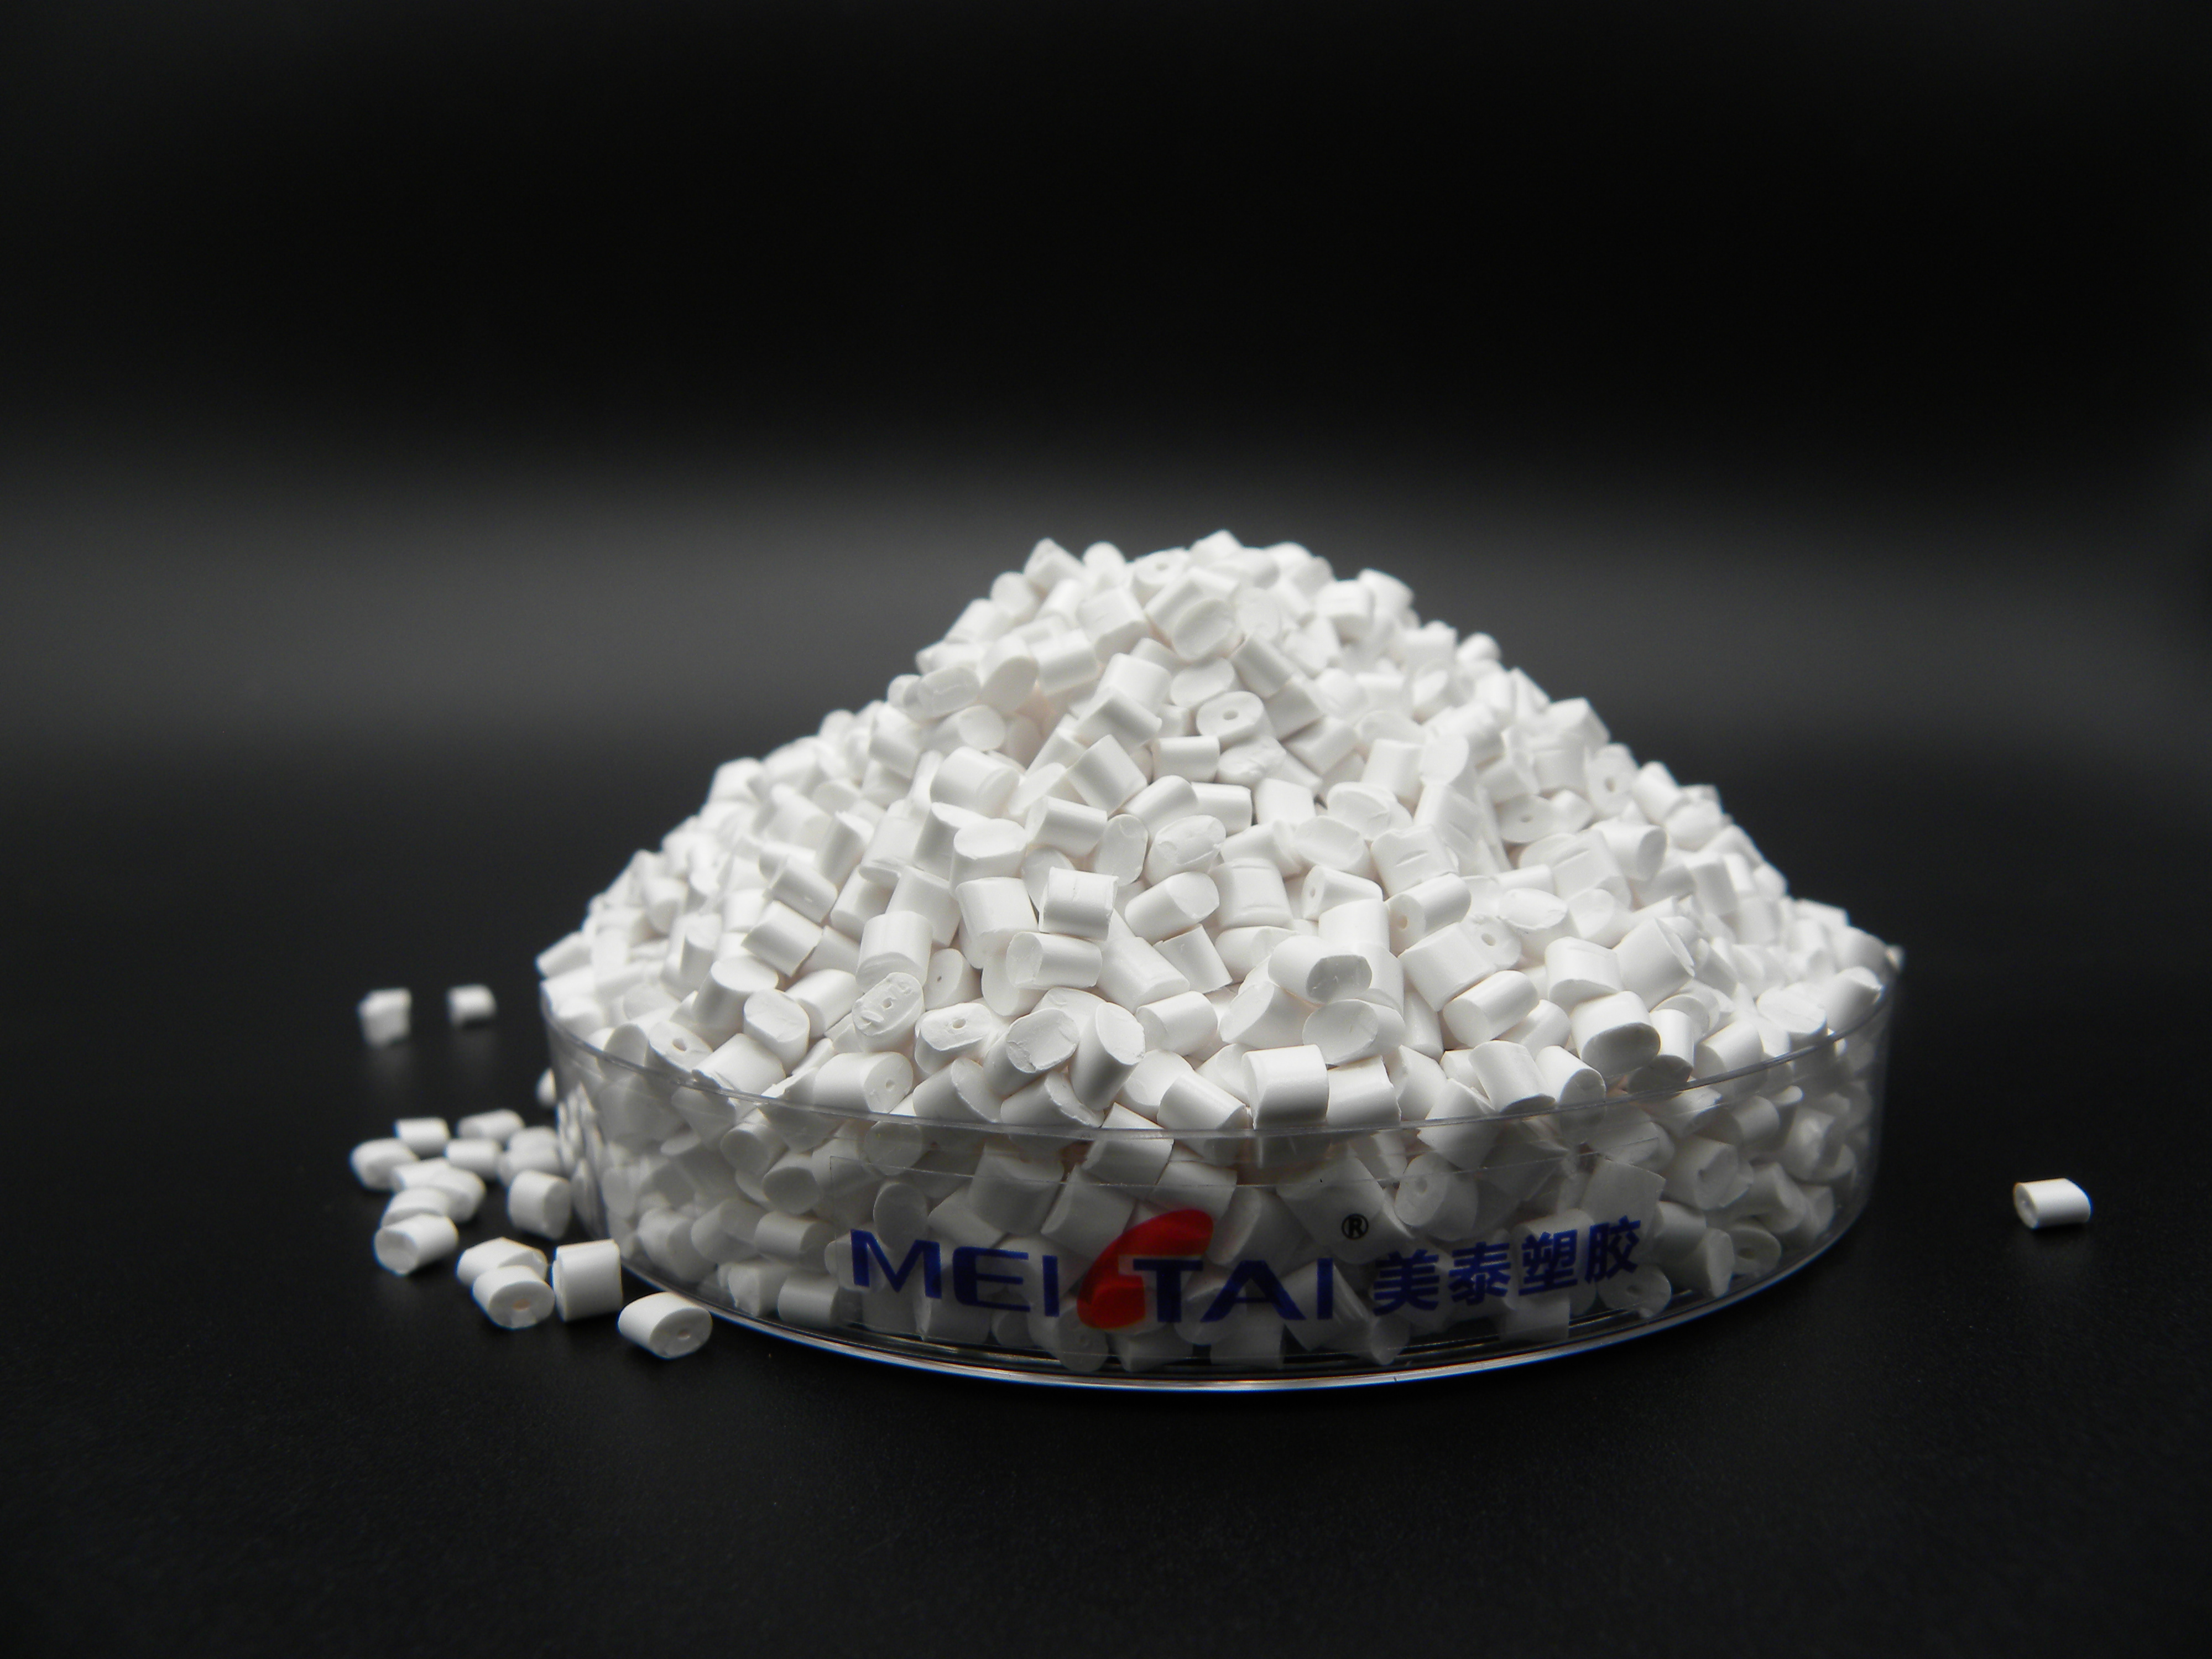
Reading PA-757 A01 as a Benchmark, Not a Specification
Chimei PA-757 A01 occupies the general-purpose, high-gloss segment. Its published property envelope is not extreme in any single direction, which is precisely why it has become a useful reference. Data from Material Data Center lists a melt flow index of 1.8 g/10 min (200°C/5 kg, ASTM D1238), a notched Izod impact of 198 J/m at 1/8 in, a flexural modulus of 2,600 MPa (ASTM D790), and a density of 1,060–1,070 kg/m³. Supplier datasheets sometimes report 1.6 g/10 min and 210 J/m at 3.2 mm, reflecting differences in test standard or lot sampling rather than a different material family. Qualifying a dye colour ABS grade against PA-757 A01 requires reading the benchmark in those terms—by test condition and thickness, not by a single headline number.
| Property | PA-757 A01 reference (ASTM/ISO) | What to confirm on the dye colour grade | Processing consequence |
|---|---|---|---|
| Melt flow | 1.8 g/10 min (200°C/5 kg); MVR 18 cm³/10 min (220°C/10 kg) | Same-condition measured value; deviation beyond 0.3–0.4 units warrants a mold-fill review | Cavity balance in multi-drop tools; shear heating in hot-runner systems |
| Notched impact | 198 J/m (1/8 in); 17 kJ/m² (Charpy, 23°C) | Same thickness and test standard | Boss cold-impact and drop-test margin |
| Flexural modulus | 2,400–2,600 MPa | Companion shrinkage data at the intended wall section | Snap-fit dimensional retention; assembly gap control |
| Density | 1,060–1,070 kg/m³ | TiO₂ loading and its effect on part weight | Kilogram price is not bill-of-material cost |
| Colour coordinates | L* 92, b* near neutral (CIE) | Pre-dye L*a*b* baseline and Δb* after dwell | Yellow shift under residence-time variation |
White pigmentation raises density through TiO₂ loading. A dye colour grade running at 1,070 kg/m³ against a 1,060 kg/m³ reference adds roughly 1% to part weight at equal volume. That figure is small in isolation but compounds across high-volume programs. The practical consequence is that a unit-price advantage of 7% cannot be validated on the resin price alone; it has to be checked against the volumetric consumption of the actual part.
Where Dye Colour ABS Fails Before It Reaches the Molding Floor
The dominant failure mode in white appliance housings is not mechanical collapse. It is colour drift that passes incoming inspection and fails at the customer's light booth or after a few months of field exposure. Third-party weathering protocols for appliance-grade ABS illustrate the scale of the requirement: colour stability is commonly assessed against ΔE ≤ 2.0, with UV blocking ≥ 95% and a yellowness index ≤ 3 under ASTM D2244. For high-visibility parts, internal colour-acceptance criteria are tighter still—ΔE ≤ 1.0 for general appearance parts and ≤ 0.8 for colour-sensitive components, with separate warning limits on ΔL, Δa, and Δb so that a passing composite score does not mask a directional drift.
UV-stable dye colour ABS for appliance exteriors depends on two variables that a pellet datasheet rarely captures: dispersion quality of the TiO₂ and stabilizer package, and the thermal history the compound sees during dye colour compounding and molding. Poor TiO₂ dispersion produces localized chalking and uneven gloss loss under QUV; an under-stabilized system may show an acceptable initial b* value but drift toward yellow after five hundred hours of UVB exposure. From experience supplying appliance molders, the lots that generate complaints are rarely the ones with a wrong initial colour match. They are the ones where b* moves between the first shot and the last shot of a production run because the melt temperature or residence time shifted outside the validated window.
A further complication sits in the supply chain itself. PA-757 chemistry is available through multiple production channels, including Taiwan-origin material, mainland China-produced 757K under the same technical system, and third-party compounded versions built on Chimei base resin. These versions can be close enough in property space to be interchangeable in many applications, but their packaging identification and lot traceability differ. White dye colour ABS lot-to-lot consistency begins with knowing which channel the material came through and whether the supplier's certificate of analysis references the same test conditions as the qualification sample.
A Four-Step Qualification Path for Dye Colour ABS
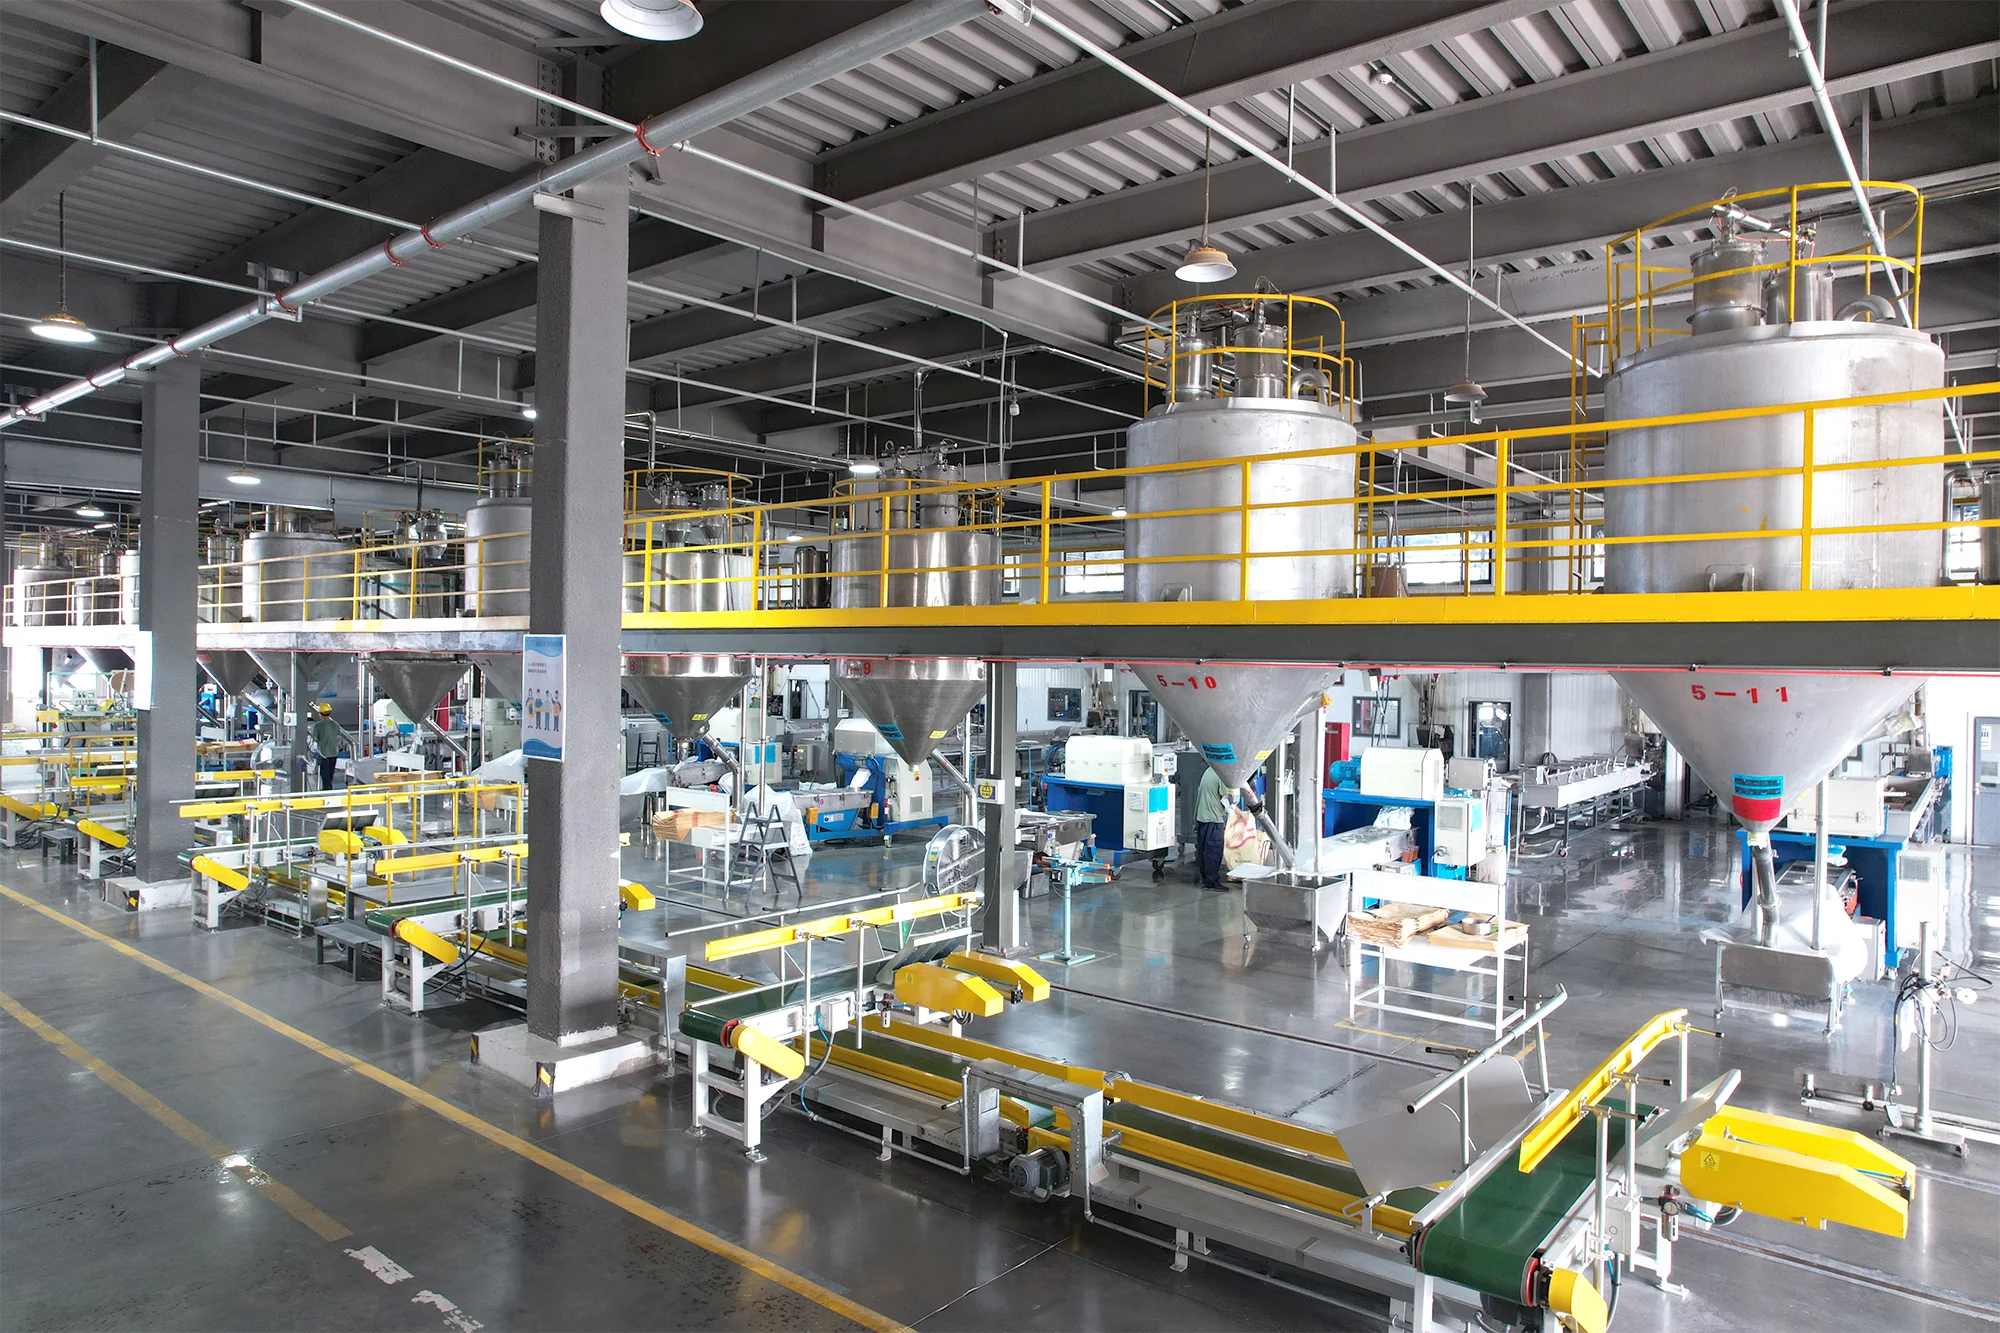
Our sister compounding operation, Qingdao Primetech Plastics, runs dye colour development and modification on engineering plastics, which gives us visibility into where qualification protocols tend to break. The sequence below is the one we recommend to appliance molders moving from a reference grade to a dye colour alternative.
| Step | Action | What to measure | Release criterion |
|---|---|---|---|
| 1 | Establish the PA-757 A01 baseline on the target press | Actual melt-flow response and L*a*b* under the production cycle | A written baseline; without it, "match" is undefined |
| 2 | First-shot trial on the same tool and colour chip | Flow-front hesitation, boss-root stress whitening, surface gloss uniformity | Cosmetic and fill acceptance before any aging test |
| 3 | Residence-time colour-shift test | b* after 5 min and 10 min of additional dwell at melt temperature | Drift band agreed with the molder, not a single-point pass |
| 4 | Pilot lot covering one full production batch | Within-cavity ΔE spread and lot-to-lot ΔE range | Consistency proven over a batch, not over a shot |
Step 3 is the one most often skipped and the one that predicts field failures most reliably. White dye colour ABS is sensitive to shear and thermal history; a grade that holds ΔE ≤ 0.8 in a short-shot trial can move outside that window when the press pauses for a break or the hot-runner setpoint drifts. Step 4 addresses a separate risk: multi-cavity colour variation. In a 4- or 8-drop tool, different cavities see different shear and cooling histories, and the resulting ΔE spread can become a batch-acceptance dispute even when the material certificate is clean.
Dye colour ABS samples from our compounding line are supplied as paid samples that are credited against subsequent orders, which keeps the trial lot traceable to a production batch rather than a hand-mixed laboratory quantity. Standard dye colours and base modifications run on a three-day sample, seven-day delivery cycle. UV-stable white dye colour ABS qualification works best when the sample itself carries the same dispersion and stabilization profile as the commercial lot.
Conclusion
PA-757 A01 remains a useful benchmark because its property envelope is moderate and well documented, not because it represents an absolute performance ceiling. A dye colour ABS grade intended for white appliance housings should be judged against that benchmark by same-condition melt flow, impact at the specified thickness, shrinkage-consistent modulus, and a dye colour system that holds ΔE through dwell and UV exposure. The qualification path is straightforward: lock the baseline, run the tool, test residence-time drift, and verify a full batch. For programs where supply continuity and colour consistency carry equal weight, working with a distributor that maintains bonded and general-trade inventory across multiple warehouses—and with an affiliated compounding operation that controls dispersion and stabilization at the pellet level—shortens the gap between a datasheet match and a production release.