 English
 Korean


How to Choose the Right Sealant Resin for BOPP Film
Selecting the right sealant resin for BOPP film is essential to achieving reliable package sealing, stable production, and the required appearance of the finished film. The sealing layer must form a secure bond within the available temperature and pressure range while remaining compatible with coextrusion, biaxial orientation, and downstream converting processes. A resin with a low seal initiation temperature may improve packaging-line efficiency, but this property alone does not determine overall performance. Film structure, hot tack, seal strength, optical quality, additive design, and end-use conditions all need to be considered. This guide explains the main selection criteria and reviews several polypropylene grades relevant to heat-sealable film applications.
1. Understand the Function of the BOPP Sealant Layer
Biaxially oriented polypropylene (BOPP) film is commonly produced through a process involving extrusion, stretching in the machine direction, and stretching in the transverse direction. Depending on the intended application, the finished film may have a single-layer or multilayer structure.
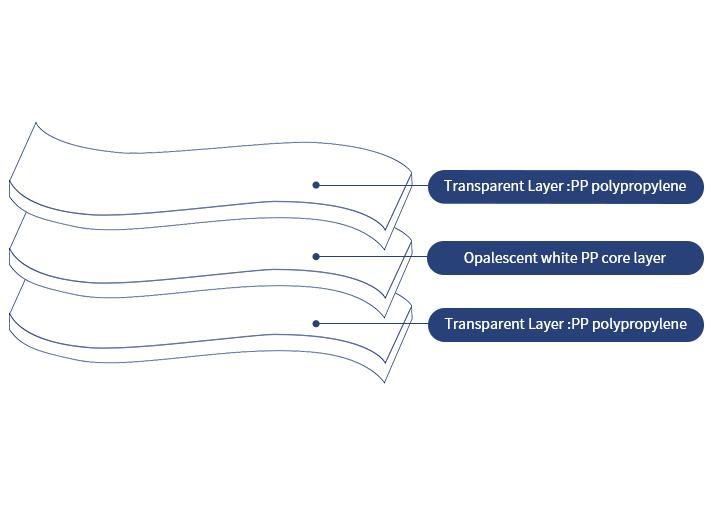
In a typical coextruded three-layer BOPP structure, the core layer provides much of the film's stiffness and mechanical integrity, while one or both outer skin layers are designed to meet specific surface requirements.
A common functional arrangement is:
The sealant resin is therefore not simply another polypropylene grade. It is a functional material that must work as part of the complete film structure.
For example, a BOPP film used for snack packaging may require reliable sealing at high packaging speeds. A metallizable BOPP film may place additional emphasis on surface quality, coating compatibility, and the additive package. These applications can require different resin characteristics even when both films use a polypropylene-based sealing layer.
2. Key Properties to Evaluate When Selecting a BOPP Sealant Resin
2.1 Seal Initiation Temperature (SIT)
Seal initiation temperature, or SIT, is one of the most important parameters when evaluating a BOPP heat-seal layer.
It indicates the temperature at which a measurable seal begins to form under a defined test method and set of conditions. A lower SIT can allow a packaging machine to create a seal at a lower jaw temperature, potentially reducing the thermal load on the film and supporting higher operating speeds.
However, SIT values should only be compared when the test conditions are sufficiently similar.
Relevant variables include:
A resin with a low reported SIT does not automatically guarantee a strong seal under every packaging condition. The actual sealing window and the required seal strength must also be evaluated.
2.2 Hot Tack Performance
Hot tack refers to the strength of a seal while it is still hot, before it has fully cooled.
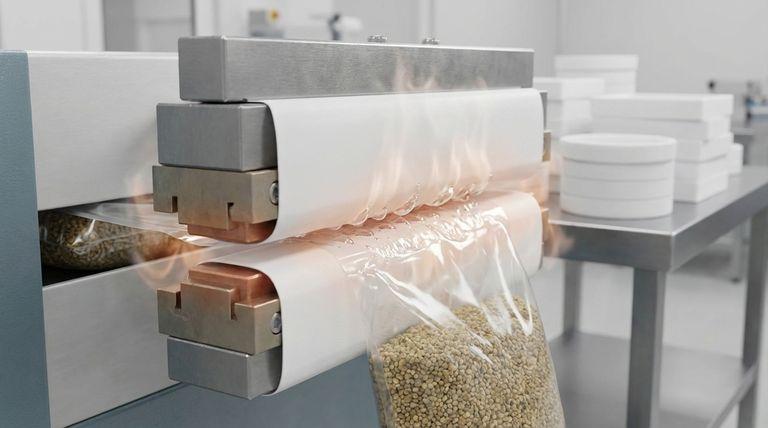
This property is particularly important in vertical form-fill-seal (VFFS) and horizontal form-fill-seal (HFFS) packaging. After a package is sealed, the film may experience mechanical stress from the product weight, filling operation, or subsequent handling.
If the hot seal cannot withstand this stress, the package may open or deform before the seal has cooled sufficiently.
When selecting a resin for high-speed packaging, evaluate hot tack curves over the relevant temperature range rather than relying on one isolated measurement.
2.3 Final Heat Seal Strength
Final heat seal strength describes the integrity of the seal after cooling. It affects package security, resistance to handling damage, and the consistency of the finished package.
A suitable sealant resin should provide sufficient seal strength without requiring excessive sealing temperature or dwell time.
The required performance depends on the packaging format, product weight, film construction, and sealing equipment. A lightweight overwrap and a heavier pouch do not necessarily require the same seal performance.
2.4 Melt Flow Rate and Processing Compatibility
Melt flow rate (MFR) is commonly used as an indicator of polymer melt flow behavior under specified test conditions.
For polypropylene, MFR is typically reported at 230°C under a 2.16 kg load, but the exact conditions should always be checked.
MFR can help engineers assess whether a candidate resin is compatible with the intended extrusion and coextrusion process. However, it should not be used alone to predict film quality.
Other factors, including molecular weight distribution, melt strength, rheological behavior, processing temperature, and the characteristics of the production line, also influence performance.
The selected sealant resin should be evaluated under the actual extrusion and orientation conditions used by the film manufacturer.
2.5 Optical Properties and Surface Quality
For transparent BOPP packaging, haze, gloss, and surface appearance are important selection criteria.
A sealant resin should be compatible with the optical requirements of the finished film. Additives, resin formulation, processing conditions, and the resulting film morphology can all influence appearance.
For metallized BOPP, surface quality becomes especially important because the outer layer may serve as the substrate for a deposited metal coating.
The appropriate resin should therefore be selected according to the specific metallization process and the required surface characteristics, rather than assuming that every low-SIT grade is suitable for metallizable film.
2.6 Additive Design
Slip and antiblock additives are commonly used to improve film handling and reduce blocking during winding, storage, and converting.
However, additive selection needs to be considered alongside the intended surface treatment and downstream process.
For example:
A resin with no technical additives may be appropriate when the film producer wants to control the additive package independently. In other cases, a pre-formulated grade may simplify production.
The correct choice depends on the film design and converting requirements.
3. Comparing Common Resin Options for BOPP Heat-Seal Layers
Polypropylene random copolymers and terpolymers are frequently considered for heat-sealable film applications.
Their suitability depends on the balance of sealing temperature, mechanical properties, optical performance, and processing behavior.
| Resin type | Typical characteristics | Selection considerations |
|---|---|---|
| PP homopolymer | Higher stiffness and a relatively high melting point | Commonly used for BOPP core layers; generally not the first choice when a low-temperature heat-seal skin is required |
| PP random copolymer | Modified crystallization and sealing behavior compared with homopolymer | May be considered where the required sealing performance and film structure are compatible |
| PP terpolymer | Can be formulated to provide lower seal initiation temperatures and specific film-sealing characteristics | Commonly evaluated for BOPP heat-seal layers |
| Modified polyolefin systems | Properties depend on the formulation and polymer composition | May be considered for specialized sealing or functional requirements, subject to compatibility testing |
A terpolymer is often a practical starting point when a BOPP producer needs a dedicated heat-sealable skin layer. Nevertheless, the word "terpolymer" alone does not establish suitability. The manufacturer's application recommendations and the grade's technical documentation should be checked.
3.1 INEOS ELTEX® P KS357: A Grade for Metallizable BOPP
For metallizable BOPP applications, INEOS ELTEX® P KS357 is a relevant grade to evaluate.
The manufacturer's product information identifies KS357 as a polypropylene heat-seal terpolymer for BOPP film, with a stated seal initiation temperature of 105°C and an application focus on metallizable film.
The available product technical information for KS357 reports:
| Property | Typical value | Test condition or method |
|---|---|---|
| Melt flow rate | 5 g/10 min | 230°C / 2.16 kg, ISO 1133-1 |
| Density | 895 kg/m³ | 23°C, ISO 1183-1 |
| Flexural modulus | 620 MPa | 23°C, ISO 178 |
| Tensile strength at yield | 20 MPa | 23°C, ISO 527-1/-2 |
| Melting point | 131°C | ASTM D3417 |
| Heat seal threshold | 105°C | 1 s, 3 bar, 100 mm/min, 100 g/cm; INEOS method |
These are typical technical data, not guaranteed specifications. The heat-seal threshold is method-dependent and should not be treated as a universal packaging-machine operating temperature.
KS357 is particularly relevant when the design requires a polypropylene terpolymer sealing layer for coextruded metallizable BOPP film. Its grade-specific application positioning makes it more directly relevant to this use than a general-purpose CPP sealant grade.
Film producers should still validate seal strength, hot tack, metallization performance, and processing stability on their own equipment.
3.2 LyondellBasell Adsyl™ 5C33F
LyondellBasell Adsyl™ 5C33F is another grade worth considering in a BOPP sealant resin evaluation.
Available product documentation describes it as an advanced polyolefin designed for use as a sealing or metallized layer in coextruded film applications. The documented processing methods include BOPP, cast film, and double-bubble film.
The published product information reports an MFR of 5.5 g/10 min at 230°C/2.16 kg and a seal initiation temperature of 105°C under the manufacturer's internal method.
Its documented application profile makes it a useful supplementary comparison when evaluating low-temperature heat-seal materials for coextruded films.
As with any alternative grade, compare the complete test conditions and application requirements rather than selecting solely on the basis of the reported SIT.
3.3 LyondellBasell Adsyl™ 5C30F
Adsyl™ 5C30F has historically been described as a BOPP sealing-layer material with low sealing temperature, optical characteristics, and suitability for metallized film.
However, available third-party material records flag this grade as discontinued. Its current commercial status should therefore be confirmed directly with the manufacturer or through current supply documentation before it is considered for a new production specification.
It is more appropriate to treat 5C30F as a historical technical reference than to assume that it is a currently available replacement option.
3.4 Hanwha TotalEnergies TF451, TF403, and TF402
Hanwha TotalEnergies offers several polypropylene terpolymer grades for heat-sealable film applications, including TF451, TF403, and TF402.
Their application positioning needs to be distinguished from BOPP-specific grades.
The manufacturer's product information identifies TF451 for film, CPP film, and lamination film applications. Its product leaflet describes it as a propylene-ethylene-butene terpolymer for aluminum-metallized cast film, with low-temperature heat sealing, transparency, gloss, stiffness, and antiblocking characteristics.
The manufacturer's product information also lists TF403 and TF402 for CPP film and thermal adhesive film applications.
These grades may be relevant when evaluating CPP or related cast-film structures. They should not automatically be treated as direct BOPP substitutes without confirmation from the manufacturer and validation on the intended BOPP production line.
4. Match the Sealant Resin to the BOPP Film Application
The intended application should guide the final material selection.
4.1 General Food Packaging Film
For general food packaging, the sealing layer needs to provide reliable sealing performance while maintaining the required optical quality and film handling characteristics.
Key considerations include:
Do not assume that a resin is automatically suitable for food-contact applications because it is used in packaging film. Confirm the relevant regulatory documentation for the specific grade, market, and final application.
4.2 High-Speed VFFS and HFFS Packaging
High-speed packaging places greater demands on the sealing window and hot tack performance.
The sealing layer needs to form a reliable bond within the available dwell time and temperature range.
A useful evaluation should include:
A low SIT can be beneficial, but it should not be used as the only indicator of high-speed packaging performance.
4.3 Metallized BOPP Film
Metallized BOPP requires additional attention to the surface characteristics of the layer receiving the metal coating.
Important considerations include:
For this application, a grade with explicit manufacturer documentation for metallizable BOPP is preferable to a grade whose application is limited to cast film or CPP.
INEOS ELTEX® P KS357 is one grade that can be evaluated in this context because its manufacturer information specifically identifies metallizable BOPP film applications.
5. How to Validate a BOPP Sealant Resin Before Production
Technical datasheets help narrow the options, but they cannot replace production validation.
A structured evaluation should include the following steps.
Step 1: Review the Technical Datasheet
Check the polymer type, MFR, density, thermal properties, recommended applications, additive information, and relevant regulatory documentation.
Confirm that the document refers to the exact grade being purchased.
Step 2: Check the Film Structure
Define whether the material will be used as a sealing skin, a metallizable layer, or another functional layer.
Confirm the layer thickness, core resin, coextrusion configuration, and orientation process.
Step 3: Evaluate Heat-Seal Curves
Measure seal strength over a range of sealing temperatures using consistent dwell time and pressure.
Identify the temperature range that provides the required seal performance rather than focusing only on the lowest temperature at which a seal can be detected.
Step 4: Measure Hot Tack
For high-speed packaging applications, evaluate hot tack at relevant temperatures and times after sealing.
The test should reflect the actual packaging process as closely as practical.
Step 5: Conduct Line Trials
Run the candidate resin under the intended extrusion, orientation, winding, and converting conditions.
Observe process stability, film appearance, blocking behavior, and sealing consistency.
Step 6: Confirm End-Use Requirements
For food packaging or other regulated applications, check the relevant compliance documents and ensure that the final film structure and intended use meet applicable requirements.
6. Common Mistakes When Choosing a BOPP Sealant Resin
Several selection mistakes can lead to poor sealing performance or unnecessary production adjustments.
Choosing a resin based only on SIT: A low SIT does not guarantee sufficient hot tack or final seal strength.
Comparing data from different test methods: Heat-seal results depend on test conditions. Values from different methods may not be directly comparable.
Ignoring additive design: Slip and antiblock additives can affect film handling and downstream surface processes.
Confusing BOPP and CPP applications: Both may use polypropylene terpolymers, but their processing routes and grade requirements are not interchangeable by default.
Selecting a grade without checking its current status: Historical datasheets and third-party product listings do not necessarily confirm current commercial availability.
Skipping production trials: Laboratory measurements provide useful screening information, but actual film-line and packaging-line validation remains essential.
Conclusion
Choosing the right BOPP sealant resin requires a balanced evaluation of seal initiation temperature, hot tack, final seal strength, processing compatibility, optical quality, and additive design. For metallizable BOPP, grades with explicit manufacturer support for that application deserve particular attention. INEOS ELTEX® P KS357 is one such grade to evaluate, while other polypropylene film grades should be assessed according to their documented application scope and current technical information. The final selection should always be confirmed through consistent laboratory testing and production trials.